


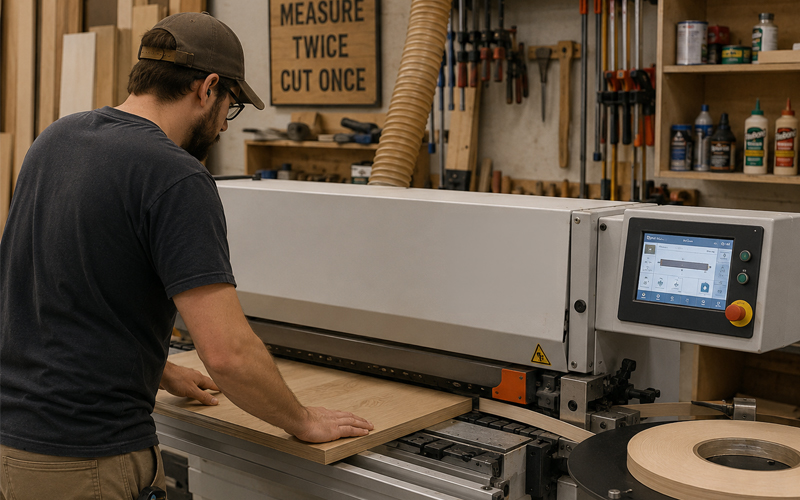
Walk through any high-performing cabinet shop, millwork facility, or kitchen and bath operation, and the edgebander is rarely the machine getting the attention—but it's almost always the one running the longest hours. While panel saws and CNC routers get the spotlight, it's the edgebander that determines whether a finished cabinet looks factory-tight or amateur. Getting this single machine right has an outsized effect on production speed, material costs, and the kind of premium work a shop can take on.
Why Edgebanding Deserves More Attention Than It Gets
Plywood, MDF, and particleboard all share one weakness: an exposed edge. Left bare, that edge absorbs moisture, chips under normal handling, and exposes the unglamorous internal layers of the panel. Edgebanding seals that edge with a thin strip of PVC, ABS, wood veneer, or laminate, bonded under heat and pressure. It is a small step with an outsized impact on durability, safety, and first impressions.
For shops serving cabinet makers, furniture builders, closet and storage companies, millwork manufacturers, and kitchen and bath specifiers, edgebanding quality is often the first thing a client notices and the last thing they forget. A few of the practical benefits at stake:
- Moisture and impact protection — sealed edges resist swelling, chipping, and delamination over years of daily use
- A finished, professional appearance — banded edges hide the raw substrate and make even budget-grade material look upscale
- Safer handling — smooth edges eliminate the splinters and sharp corners that come with raw panel stock
- Pricing power — clean, consistent edges are one of the easiest details for clients to judge quality by, which supports premium pricing on finished work
The labor math tells the real story. Hand-applying edge tape with an iron and a roller is workable for the occasional repair or one-off piece, but it does not scale. Shops that move from manual application to an edgebanding machine consistently report dramatic gains—anywhere from 300% to 400% in throughput compared to manual methods, according to industry data compiled by the Woodworking Network. That kind of gain is the difference between edgebanding being a bottleneck and edgebanding being a non-issue.
Edgebanding Materials and Adhesives: What's Actually Holding the Edge On
Before comparing machines, it helps to understand what the machine is actually doing. Two variables drive almost every decision in edgebanding: the banding material and the adhesive that bonds it.
Banding Materials
- PVC and ABS edgebanding — durable, available in nearly unlimited colors and finishes, and the standard choice for laminate and melamine casework
- Wood veneer edgebanding — used when the panel face is real wood veneer or solid lumber and the edge needs to match grain and color
- Solid wood strips — thicker (often 3-5mm), used where the edge will see heavy wear, such as worktops and high-traffic furniture edges
Adhesive Systems: EVA vs. PUR
Most edgebanders apply a hot-melt adhesive from a heated glue pot. The two dominant chemistries are EVA (ethylene-vinyl acetate) and PUR (polyurethane reactive), and the difference between them matters more than most shops realize when they're shopping for a machine.
EVA is a thermoplastic adhesive: it melts when heated and solidifies again as it cools, forming a strong bond once the heat is removed. It's the workhorse of the industry—affordable, easy to run, and forgiving for everyday casework. PUR, by contrast, cures through a chemical reaction rather than simple cooling. PUR adhesive holds up far better under heat, resisting melting or losing its bond even at temperatures up to roughly 150°C, which is why it has become the standard for kitchens, bathrooms, and anywhere moisture and heat are a daily concern.
If a shop is producing general residential casework, closets, or shelving where cost matters more than extreme moisture resistance, EVA is usually the right call. If the work is headed for kitchens, bathrooms, commercial food service, or anywhere the finished piece will see water and temperature swings, PUR is worth the added cost and maintenance. As one industry adhesive supplier puts it, when joints need to be water or heat resistant—fire doors or kitchen cabinets—PUR adhesive is the recommended choice, since it offers significantly higher water and heat resistance than EVA.
The tradeoff with PUR is upkeep. Because it cures chemically rather than just cooling, leftover PUR glue can set up inside the machine if it sits idle too long, which means more disciplined cleaning routines. Many modern edgebanders now offer hybrid glue pots that switch between EVA and PUR, giving shops the flexibility to run both without owning two machines.
Edgebander Types: Matching the Machine to the Shop
Edgebanders span an enormous range, from countertop units a single operator can run by hand to fully automated lines that feed, glue, trim, and buff hundreds of panels per shift. Understanding where a shop sits on that spectrum is the first step in choosing the right edgebander.

Operator-fed machines that handle glue application, pressing, and trimming, while the operator guides the panel. A strong fit for shops running fewer than a few hundred linear feet of edge per day.
View Manual Edgebanders
Chain or belt-fed machines that move panels through gluing, pressing, end trimming, and top/bottom trimming automatically. The standard for shops producing daily volume.
View Automatic EdgebandersPortable Edgebanders for On-Site and Renovation Work
For remodel companies and shops that frequently work on-site, portable edgebanders fill a specific niche. They let a crew band a replacement drawer front, a damaged cabinet door, or a custom shelf without hauling the piece back to the shop. It's a slower process than a production-line machine, but for renovation and field service work, the time saved on transport alone often justifies the investment.
Pre-Milling and Corner Rounding: Where the Real Time Savings Live
Two features separate a basic automatic edgebander from one that genuinely reduces labor: pre-milling and corner rounding. Pre-milling lightly trims the panel edge immediately before the banding is applied, removing saw marks and squaring the surface so the bond is tight and even. Corner rounding automatically trims the front and back corners of the banding flush with the panel, a step that otherwise requires hand-sanding every single corner of every single piece.
For a shop running dozens of cabinets a week, those two features alone can eliminate hours of hand-finishing work per day.
| Feature | What It Does | Who Needs It |
|---|---|---|
| Pre-Milling | Trims the raw panel edge before banding for a tighter, cleaner bond | Shops cutting on a panel saw with slight blade marks or chipping |
| Corner Rounding | Automatically trims and rounds banding corners flush to the panel | Shops that currently hand-sand every corner |
| Digital/CNC Controls | Stores programs for panel thickness, edge thickness, and pressure settings | Shops switching between multiple edge materials and thicknesses daily |
| Return Conveyor | Feeds finished panels back to the infeed side automatically | One- or two-person operations needing continuous feeding without extra labor |
Glue-Less Edgebanding: Hot Air and Laser Fusion
A newer category of edgebander skips the visible glue line entirely. Instead of a traditional glue pot, these machines use specialized banding with a pre-applied adhesive layer, then melt that layer with hot air or a laser/infrared source at the moment the banding is pressed onto the panel. The result is a joint with no visible seam at all—a detail that high-end kitchen and furniture clients notice immediately.
These systems cost more and require dedicated banding material, so they tend to make the most sense for shops competing on premium finish quality rather than raw volume. For a shop fielding regular requests for an "invisible edge" look, the upgrade can become a genuine differentiator in a competitive bid.
Sizing an Edgebander to Shop Volume
Matching machine capability to actual production volume avoids two expensive mistakes: under-buying a machine that becomes the shop's bottleneck, or over-buying capacity that never gets used.
- Fewer than a few hundred linear feet of edge banding per day
- Best fit: a compact automatic edgebander with basic end and top/bottom trimming, or a portable unit for field work
- Priority: ease of operation and a small footprint over raw speed
- Steady production of multiple kitchens, vanities, or casework runs per week
- Best fit: an automatic edgebander with pre-milling, corner rounding, and digital program storage for fast changeovers
- Priority: minimizing setup time between different edge thicknesses and materials
- Continuous production across multiple shifts
- Best fit: industrial single-sided automatic edgebanders with multi-axis trim control, return conveyors, and optional hot-air or PUR capability
- Priority: uptime, durability, and integration with upstream panel saw or CNC router workflows
One regional kitchen and bath manufacturer replaced a manual edgebanding station with a mid-range automatic unit featuring pre-milling and corner rounding. Within the first year, the shop reported being able to take on noticeably more cabinet orders without adding finishing labor, while warranty callbacks related to chipped or lifting edges dropped substantially.
The Economics: Why Edgebanding ROI Adds Up Quickly
The cabinetry market is not slowing down. Industry analysts project the global cabinet market will grow from roughly $141 billion in 2025 to nearly $190 billion by 2031, driven by remodel activity and rising demand for frameless, modular cabinet construction. At the same time, a majority of kitchen and bath firms report moderate to severe labor shortages, which is pushing more shops toward automation to protect throughput and consistency without expanding headcount.
For shops weighing the investment, a few numbers consistently come up in the field:
- Manual edge taping: roughly 1-2 minutes per linear foot, plus hand-finishing time for every corner
- Basic automatic edgebander: 8-15 meters per minute feed rate, depending on the machine and material
- Mid-range to industrial automatic edgebander: 15-25+ meters per minute, with pre-milling and corner rounding eliminating most hand-finishing
Against that backdrop, edge banding waste is a smaller factor than most shops assume—industry data suggests it accounts for only a modest share of total material waste in panel processing—which means the bigger savings almost always come from labor, not material.
Setting Up an Edgebander for Long-Term Reliability
An edgebander is a precision machine, and like any production equipment, it rewards a proper setup and routine maintenance. A few non-negotiables worth building into daily and weekly routines:
- Keep glue pot temperatures calibrated—overheated EVA scorches and weakens the bond, while underheated glue won't flow evenly
- Check pressure rollers and trim cutters weekly; dull cutters are one of the most common causes of chipped or rough banding
- Run test pieces after any changeover in material thickness or banding type before starting a full production run
- Keep dust collection dialed in near the trim units—fine trim dust is abrasive and accelerates wear on cutting heads
- If running PUR adhesive, follow the manufacturer's flushing and cleaning schedule precisely; leftover PUR that cures inside the pot is far more difficult to remove than EVA
Common Edgebanding Problems and What's Usually Behind Them
Almost always traced to dull trim cutters, an incorrect feed rate, or a panel edge that wasn't square going into the machine. Pre-milling solves a large share of these issues by cleaning up the edge before banding is even applied.
Usually a sign of too much glue, the wrong adhesive temperature, or a mismatch between banding thickness and glue pot settings. Switching to PUR, or to a hot-air glue-less system, can largely eliminate this issue for shops where an invisible seam matters to clients.
Often a moisture or heat resistance problem—EVA simply isn't built for high-humidity kitchen and bath environments the way PUR is. If lifting becomes a recurring callback issue, it's usually a sign the shop has outgrown its current adhesive system.
An edgebander rarely gets the attention a CNC router or panel saw does, but it's frequently the machine running the most hours and shaping how a finished piece is judged. Whether a shop needs a simple manual unit for occasional work or a fully automated line with pre-milling, corner rounding, and PUR capability, the right choice comes down to matching machine capability to real production volume and the durability demands of the finished product.
For cabinet makers, millwork manufacturers, kitchen and bath companies, and construction firms looking to scale, the right edgebander is rarely a luxury upgrade—it's one of the fastest ways to protect margins, reduce callbacks, and take on more work without adding labor.
 Dust Collectors
 Sliding Table Saws
 Dovetail Machines
 Cantek
 SCM
